Industrial vacuum needs show up across very different processes — drying, distillation, filtration, evaporation, and material transport. One technology that has served these needs for decades, especially in chemical, food, paper, and mining applications, is the liquid ring vacuum pump. This article walks through how a liquid ring vacuum pump actually works, which processes it suits best, and where its technical limits lie.
Table Of Contents
- What Is the Working Principle of a Liquid Ring Vacuum Pump?
- How Do the Rotor and Liquid Ring Create Vacuum?
- Why Can Liquid Ring Pumps Tolerate Vapor and Small Amounts of Liquid?
- What Does Near-Isothermal Compression Mean, and Why Does It Matter?
- How Do Service Liquid Temperature and Flow Affect Performance?
- What Are the Limits of a Liquid Ring Vacuum Pump?
- Which Processes Favor Liquid Ring Vacuum Pumps?
- What Is the Difference Between Monoblock, Single-Stage and Two-Stage Models?
- Frequently Asked Questions
What Is the Working Principle of a Liquid Ring Vacuum Pump?
A liquid ring vacuum pump consists of a rotor mounted eccentrically inside a cylindrical casing. The casing is partially filled with a service liquid, most commonly water. As the rotor spins, centrifugal force throws the liquid outward against the casing wall, forming a rotating ring of liquid that lines the inner surface of the casing. Because the rotor sits off-center relative to the casing, the volume between the rotor blades and the liquid ring changes continuously as the rotor turns.
This changing volume is the core mechanism behind the pump's vacuum action. As the cells between the rotor blades approach the suction port, they expand; the expanding volume lowers the local pressure and draws gas in through the inlet. As the same cells rotate toward the discharge port, they contract; the shrinking volume compresses the gas and pushes it out through the outlet. This cycle repeats with every full rotation of the rotor, producing a continuous gas flow.
How Do the Rotor and Liquid Ring Create Vacuum?
The role the liquid ring plays here is comparable to what a solid piston does inside a cylinder — except a moving liquid layer takes the piston's place. The most important consequence of this design is that the rotor blades never make metallic contact with the casing or with each other. The liquid film forms a continuous layer between moving and stationary parts, which both provides sealing and dramatically reduces wear.
This mechanical simplicity is also the main reason liquid ring pumps need relatively little maintenance. There are no gears, cams, or piston rings requiring lubrication; the only moving part is the rotor, and it turns on a film of liquid. This same principle underlies Gücüm Pompa's monoblock, single-stage, and two-stage series — what differs between them is the number of stages, the casing size, and consequently the achievable capacity and vacuum level.
Why Can Liquid Ring Pumps Tolerate Vapor and Small Amounts of Liquid?
Unlike dry-type vacuum pumps, liquid ring pumps already carry a continuously circulating liquid inside them, so a certain amount of water vapor or liquid droplets in the incoming gas stream does not disrupt operation. This makes liquid ring pumps particularly well suited to applications where moist or vapor-laden gas is simply part of the process — drying, distillation, evaporation, and filtration among them.
In a dry-type pump, a comparable situation can lead to condensation on internal surfaces, corrosion, or component damage. In a liquid ring system, the entrained vapor mixes into the service liquid and is discharged from the system in liquid phase. That reduces how tightly an operator needs to control moisture or vapor content in the process stream.
What Does Near-Isothermal Compression Mean, and Why Does It Matter?
Compressing a gas normally raises its temperature — a phenomenon known as adiabatic compression, which wastes energy and, for some gases, introduces an ignition risk. In a liquid ring vacuum pump, however, the gas stays in constant contact with the liquid ring throughout compression. The liquid absorbs most of the heat generated during compression almost immediately, preventing the gas temperature from rising sharply.
Engineers call this "near-isothermal compression" — the compression process stays close to an ideal, constant-temperature (isothermal) compression rather than a heat-generating adiabatic one. This matters for two reasons: first, it lowers temperature-related risks when handling flammable or reactive gases; second, it improves compression efficiency and limits energy consumption.
How Do Service Liquid Temperature and Flow Affect Performance?
The temperature of the service liquid is one of the factors that directly sets the maximum vacuum level a liquid ring pump can reach. The liquid's vapor pressure establishes the theoretical vacuum limit — the warmer the liquid, the higher its vapor pressure, and the more that constrains how deep a vacuum the pump can pull. This is why catalog figures are usually given at a specific reference temperature (often around 15°C); if the actual service water runs warmer than that reference in real operating conditions, the achievable vacuum will fall below the catalog value.
Service liquid flow rate matters in a similar way. Too little liquid prevents the ring from forming properly and causes a loss of vacuum, while too much liquid wastes energy and, in some cases, can even reduce pump performance. Keeping the service liquid flow within the range the manufacturer specifies is therefore a critical operating detail for both vacuum stability and energy efficiency.
What Are the Limits of a Liquid Ring Vacuum Pump?
Alongside their strengths, liquid ring vacuum pumps carry some real technical limits. The absolute vacuum level they can reach is bounded by the vapor pressure of the service liquid, so on their own they may not be enough for applications requiring very deep vacuum — sub-millibar levels, for instance. In those cases, adding a vacuum booster ahead of the liquid ring pump can push the achievable vacuum level considerably lower.
Continuous water or oil consumption and circulation is another consideration. In open-loop systems this raises water cost, and in some regions water availability itself can be a constraint. Closed-loop water-circulated or oil-circulated vacuum units address this by cooling and reusing the liquid within the system, substantially reducing this limitation.
Which Processes Favor Liquid Ring Vacuum Pumps?
Vapor and liquid tolerance, near-isothermal compression, and low maintenance needs make liquid ring vacuum pumps a preferred solution in several process categories:
- Drying and dehydration: Water vapor released from the material being dried does not compromise pump performance.
- Distillation and evaporation: Chemical and food processing rely on vacuum conditions for low-temperature distillation or concentration steps.
- Vacuum filtration: In mining and chemical applications, small amounts of liquid carried through the filter medium do not damage the pump — a significant advantage.
- Paper production: On paper machines, high-capacity liquid ring pumps remove water from the pulp in the forming and press sections.
- Packaging and transport applications: Vacuum material handling and vacuum lifting systems need stable, continuous vacuum.
Gücüm Pompa liquid ring vacuum pumps are used in the chemical, food, plastics, textile, glass-ceramic, health, paper, sugar, leather, mining, forestry, vacuum lifting, groundwater, power generation, ceramics, and defense industries.
What Is the Difference Between Monoblock, Single-Stage and Two-Stage Models?
Liquid ring vacuum pumps fall into different families depending on the number of stages and the casing design. Within Gücüm Pompa's range, that distinction looks like this:
- Monoblock design (GMVP / GMVX series): The rotor is mounted directly on the motor shaft, with no separate coupling. This means fewer parts, a more compact footprint, and simpler alignment. According to the catalog, this series covers 30–375 m3/h in capacity and reaches up to 33 mbar vacuum.
- Two-stage design (GMP / GVP series): A classic layout with two rotors operating in sequence. The catalog lists 55–2,515 m3/h in capacity and 33–40 mbar in vacuum, with a lower cavitation risk noted compared to single-stage design.
- Single-stage design (GMVT / GMPT series): Built with larger casings for applications requiring high suction capacity. According to the catalog, this series reaches 650–12,000 m3/h in capacity and 40–100 mbar in vacuum.
Choosing the right model depends on required capacity, target vacuum level, vapor load in the process, and available installation space. Sharing accurate process data with the pump manufacturer at the project stage is therefore decisive for selecting the correct pump.
Frequently Asked Questions
What Liquid Is Used in a Liquid Ring Vacuum Pump?
Water is by far the most common service liquid. In certain specialized applications, other liquids may be chosen based on process requirements. The right choice of service liquid should be made according to process conditions and the pump manufacturer's recommendations.
When Is a Liquid Ring Vacuum Pump More Advantageous Than a Dry-Type Pump?
When the gas stream is likely to carry vapor, moisture, or small amounts of liquid, a liquid ring pump has a natural advantage because it tolerates these conditions by design. For completely dry, clean gas streams requiring very deep vacuum, other pump technologies may be worth evaluating as well.
Why Might a Liquid Ring Vacuum Pump's Vacuum Level Fall Short of the Catalog Value?
The most common reason is that the service liquid runs warmer in actual operating conditions than the reference temperature used in the catalog. Insufficient service liquid flow, leaks in the suction line, or incorrect sizing can also prevent the pump from reaching its catalog vacuum value.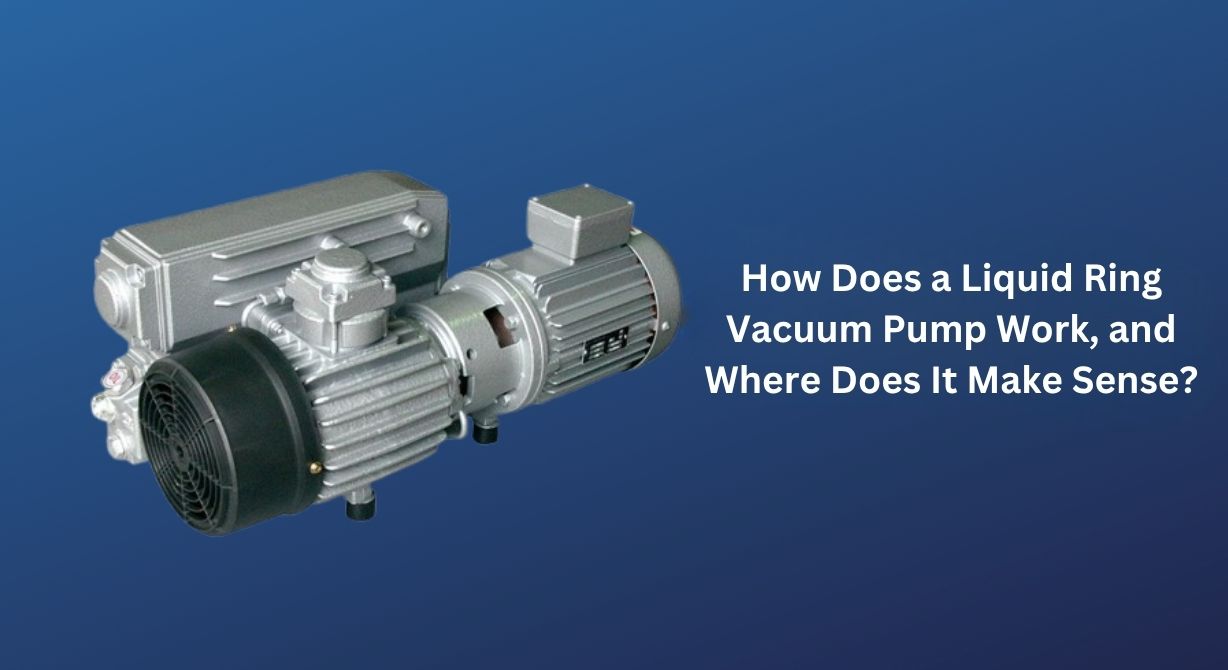
Is a Liquid Ring Pump Enough on Its Own for Processes That Need Very Deep Vacuum?
Because the service liquid's vapor pressure sets a limit on the vacuum level a liquid ring pump alone can reach, applications requiring deeper vacuum typically need a vacuum booster installed ahead of the liquid ring pump to lower the achievable vacuum level further.