In the chemical and pharmaceutical industries, vacuum forms the basis of many processes such as distillation, drying, filtration, and lyophilization. This article covers, in general terms, the role of vacuum in these sectors, material selection for aggressive gases, pump types, GMP requirements, and sealing issues. To determine the right solution for your process, you can consult the Gücüm Pompa technical team.
Table of Contents
- Why Is Vacuum Technology Critically Important in the Chemical and Pharmaceutical Industries?
- In Which Processes Is Vacuum Used in the Chemical Industry?
- What Is the Role of Vacuum in Pharmaceutical Production?
- Why Is Material Selection Decisive in the Evacuation of Aggressive Gases?
- Which Materials Stand Out in Terms of Corrosion Resistance?
- Which Types of Vacuum Pumps Are Preferred in the Chemical and Pharmaceutical Sectors?
- How Do GMP Standards Affect Vacuum System Selection?
- How Is Sealing and Safety Ensured in Aggressive Gas Applications?
- What Criteria Should Be Taken as Basis in Vacuum Pump Selection in the Chemical and Pharmaceutical Industries?
- Frequently Asked Questions
Why Is Vacuum Technology Critically Important in the Chemical and Pharmaceutical Industries?
The chemical and pharmaceutical industries are among the sectors where vacuum technology is tested under the most challenging conditions. In the chemical industry, the vacuum pump is an indispensable component for the sustainable execution of basic chemical processes such as distillation, crystallization, filtration, drying, and evaporation. Vacuum in pharmaceutical production directly affects quality, purity, and repeatability criteria across a wide range of processes from raw material synthesis to final product packaging.
Unlike standard industrial applications, vacuum systems in chemical and pharmaceutical processes are in constant contact with acid vapors, solvents, toxic gases, and reactive chemicals. Incorrect material selection or inadequate design can lead to pump failure, contamination, environmental pollution, and serious occupational safety risks. In these sectors, vacuum pump selection is not only an engineering decision but also a safety and compliance decision.
In Which Processes Is Vacuum Used in the Chemical Industry?
Distillation is one of the processes where vacuum is most intensively used in the chemical industry. Vacuum distillation is preferred for separating compounds with very high boiling points at atmospheric pressure or heat-sensitive compounds; lowering the pressure also lowers the boiling point, allowing the compound to be separated without degradation. This process is a common application in petrochemicals, fine chemicals, and aroma substance production.
In crystallization and precipitation processes, vacuum controls the solvent evaporation rate and regulates crystal size and purity level. Vacuum filtration shortens filtration time in solid-liquid separation processes and increases production efficiency. In polymer production, removal of monomers and solvents from the reaction environment, accelerating evaporation in solvent recovery units, and creating an inert gas atmosphere in chemical reactors are also among the vacuum-dependent processes of the chemical industry.
What Is the Role of Vacuum in Pharmaceutical Production?
In pharmaceutical production, vacuum is managed as a critical process parameter due to its decisive effect on product purity and stability. Many reaction steps in active pharmaceutical ingredient synthesis must be carried out in oxygen-free or low-pressure environments. The vacuum level and stability applied in these steps directly determine reaction efficiency and final product quality.
Lyophilization, or freeze-drying, is one of the most technical vacuum applications in the pharmaceutical industry. This process, which plays a critical role in ensuring the stability of biological drugs, vaccines, and sensitive protein formulations, requires maintaining extremely deep vacuum levels stably for long periods. Vacuum granulation and drying in tablet and capsule production, vacuum packaging in sterile filling lines, and pressure differential management in clean room systems are other important headings of pharmaceutical vacuum applications.
Why Is Material Selection Decisive in the Evacuation of Aggressive Gases?
Gases evacuated in chemical and pharmaceutical processes may contain extremely aggressive components such as hydrochloric acid, sulfuric acid, nitric acid, ammonia, chlorine, fluorine compounds, organic solvents, and reactive vapors. Pumps made of standard cast iron or low-alloy steel wear out rapidly in aggressive gas environments; this both significantly shortens pump life and creates contamination and leakage risks. From a process safety perspective, material selection is the primary design criterion that comes before pump type.
The body, rotor, vanes, seals, and all internal surface materials of the vacuum pump to be used in aggressive gas evacuation should be evaluated individually for compatibility with the gas composition to be evacuated. Depending on the concentration of the compound, temperature, moisture content, and process duration, different material classes may come to the fore. Chemical resistance tables provided by the manufacturer should be used as the basic reference source in this evaluation process.
Which Materials Stand Out in Terms of Corrosion Resistance?
AISI 316L stainless steel is the commonly preferred starting material for general chemical resistance requirements. Thanks to its molybdenum content, it provides significant superiority over standard 304 grade stainless steel in chloride environments. However, it may not provide sufficient protection in high-concentration acid environments; in this case, transition to higher alloy materials is necessary.
Hastelloy C276 and C22 alloys stand out as the material class preferred in the most challenging environments of the chemical industry, showing superior resistance to both oxidizing and reducing acids over a wide pH range. In processes containing fluorine compounds and hydrofluoric acid, PTFE-coated or fully PTFE-bodied pumps may be required; PTFE's chemical resistance forms a reliable barrier across a wide range of aggressive environments. Titanium is a special material option that offers high resistance especially in chloride environments and oxidizing acids, but is preferred in critical points due to its high cost.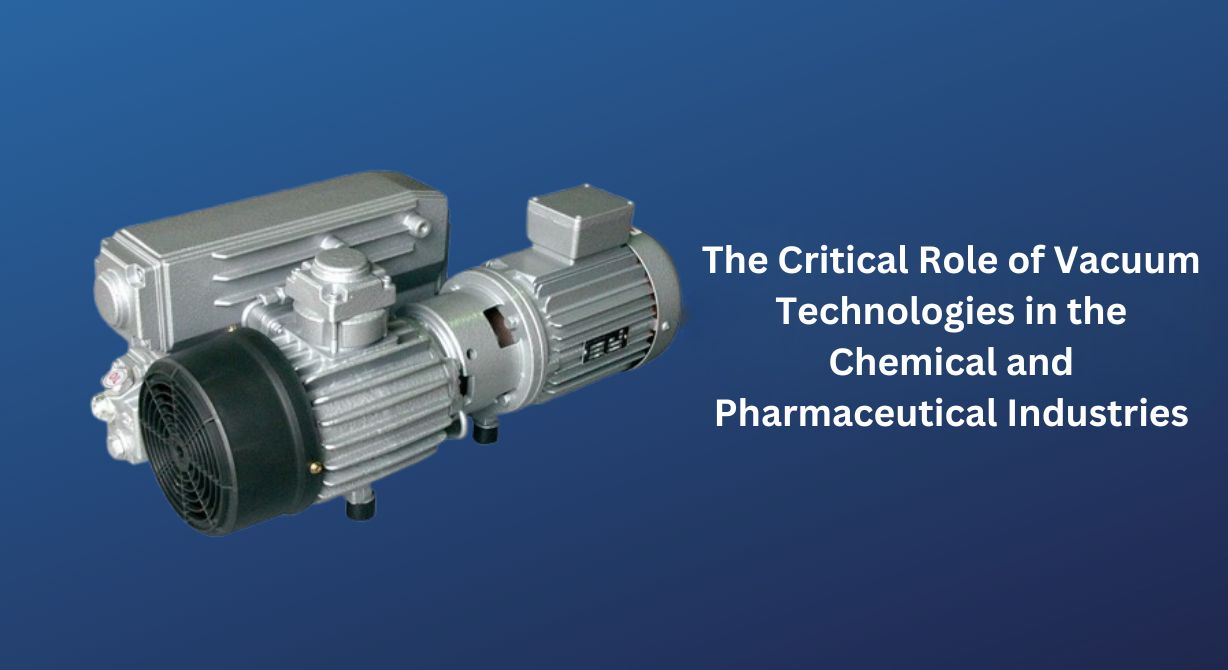
Which Types of Vacuum Pumps Are Preferred in the Chemical and Pharmaceutical Sectors?
Liquid ring vacuum pumps have been a preferred solution in the chemical industry for many years in the management of acid and solvent vapors. The ability to use water, process liquid, or a compatible liquid as the operating (sealing) liquid allows safe evacuation of condensable vapors and resistance to liquid carryover. However, the physical limitation between operating liquid temperature and achievable vacuum level restricts the pressure range where liquid ring systems are suitable.
Dry screw vacuum pumps are preferred in the pharmaceutical sector because they meet oil-free and clean vacuum requirements. These pumps, equipped with PTFE or special alloy coated screw rotors, can also operate safely in aggressive gas environments. Diaphragm vacuum pumps offer a reliable solution in terms of chemical resistance in laboratory and small-scale production applications requiring low flow and medium vacuum; the PTFE diaphragm and PTFE-coated body combination provides broad chemical compatibility. Because pump type and material selection vary by application, the suitability of Gücüm Pompa's liquid ring and other vacuum pump options for your process should be evaluated together with the technical team.
How Do GMP Standards Affect Vacuum System Selection?
Good Manufacturing Practices (GMP) standards require that every equipment used in pharmaceutical production complies with defined quality and safety parameters. The vacuum system falls within this scope; material certificates of the pump used, calibration records, cleaning and sanitization procedures, and validation documents must be prepared completely and kept available for audit processes.
In GMP-compliant vacuum systems, the gas exiting the pump must not return to the process environment, the exhaust line must be designed in accordance with environmental and safety regulations, and the vacuum level must be continuously monitored with calibrated measuring devices. FDA 21 CFR Part 11 requirements should also be considered for monitoring systems that use electronic records and signatures. Documenting all processes from equipment selection to installation, validation to routine maintenance within the GMP framework is an important safeguard against possible audit findings.
How Is Sealing and Safety Ensured in Aggressive Gas Applications?
Sealing in aggressive gas evacuation is a critical requirement not only for performance but also for occupational safety. Any leakage from the pump in systems containing toxic or flammable gases can lead to exposure risks threatening worker health, explosion hazards, and environmental pollution. Mechanical seal selection requires particularly meticulous evaluation in these applications.
Dual mechanical seal systems are the preferred safety solution in critical applications. The space between the two seals is filled with an inert barrier liquid; thus, the leakage of process gas to the atmosphere is prevented and seal wear can be monitored. Magnetically driven pumps provide a leak-free structure by eliminating the shaft seal, significantly reducing leakage risk; this design may be preferred in processes where toxic or high-value chemicals are processed. Equipping gas exhaust lines with explosion-proof connection elements and pressure relief valves is also among the complementary elements of the safety system.
What Criteria Should Be Taken as Basis in Vacuum Pump Selection in the Chemical and Pharmaceutical Industries?
Chemical compatibility analysis forms the cornerstone of the selection process. All components of the gas composition to be evacuated, their concentrations, temperature range, and condensation conditions must be fully determined; then the resistance of each pump material to these conditions should be cross-checked from the manufacturer's chemical resistance tables. Even the incompatibility of a single component requires the material configuration to be completely reviewed.
The required vacuum level and flow, sectoral regulatory requirements, cleanability, exhaust management, and after-sales technical support capacity are other decisive criteria in selection. The Gücüm Pompa technical team provides technical consultancy in determining the vacuum solution suited to the application. Equipment selection that meets long-term reliability and compliance requirements is an important part of operational sustainability in these sectors.
Frequently Asked Questions
Which Pump Material Is Recommended for Hydrochloric Acid Vapor?
In processes containing hydrochloric acid vapor, Hastelloy C276, PTFE coating, or fully PTFE-bodied pumps are preferred. In low concentrations, 316L stainless steel may be sufficient; however, compatibility must be verified from the manufacturer's chemical resistance table in high concentration and temperature.
What Documents Are Required for a GMP-Compliant Vacuum Pump in Pharmaceutical Production?
For a GMP-compliant vacuum pump, material certificates, manufacturing conformity certificate, calibration records, cleaning and sanitization procedures, and equipment validation protocol must be prepared. The technical file to be obtained from the manufacturer must support the validation process.
Which Pump Type Is Safer in Applications Containing Solvent Vapor?
In applications containing solvent vapor, liquid ring vacuum pumps offer safe evacuation by keeping condensable vapors in liquid form. If dry-type pumps are to be used, the body temperature must be kept above the solvent condensation point and the exhaust line must be connected to an appropriate recovery or disposal system.
How to Prevent Toxic Gas Leakage from the Vacuum Pump?
To prevent toxic gas leakage, dual mechanical seal systems or magnetically driven leak-free pump design should be preferred. Connecting the exhaust line to a closed and negative pressure ventilation system, continuous monitoring with gas detectors, and regular seal checks constitute the complementary elements of these safety measures.
How Is Vacuum Pump Maintenance Frequency Determined in the Chemical Industry?
Maintenance frequency depends on the aggressiveness level of the evacuated gas, operating time, and pump operating conditions. In aggressive gas environments, sealing elements and corrosion-exposed parts should be inspected and replaced more frequently than in standard applications. In addition to the manufacturer's maintenance plan, periodic performance monitoring supported by chemical analysis is recommended.