In a plastic extrusion line, vacuum serves two quite different purposes: removing volatiles from the molten polymer (degassing) and calibrating the extruded pipe or profile to its final dimensions. These two applications bring different operating conditions and different pump requirements. This article covers how each application works and why a particular pump technology is typically preferred for each task.
Table Of Contents
- What Are the Two Different Uses of Vacuum in Plastic Extrusion?
- How Does Vacuum Degassing Work in an Extruder?
- Why Is Degassing Critical for Moisture-Sensitive Polymers?
- How Does Vacuum Calibration Work in Pipe and Profile Extrusion?
- How Does the Wet Environment in a Calibration Tank Affect Pump Selection?
- Which Pump Technology Is Preferred for Degassing and Calibration?
- What Protective Measures Guard Against Melt Splashing?
- Frequently Asked Questions
What Are the Two Different Uses of Vacuum in Plastic Extrusion?
Vacuum comes into play at two fundamental points in a plastic extrusion process. First, through an opening on the extruder barrel, moisture, residual monomer, or trapped air within the molten polymer is removed — a process called "degassing" or "devolatilization." Second, the pipe or profile leaving the die is shaped to its correct dimension under vacuum in a calibration tank while it cools.
Although both applications use vacuum, their operating conditions differ considerably; the sections below cover those differences and the pump characteristics each one requires.
How Does Vacuum Degassing Work in an Extruder?
In degassing, the depth of the screw channel is increased at a specially designed zone on the extruder screw; this geometric change lowers pressure on the melt at that point, creating a vacuum connection port. A vacuum pump connected to this port draws out the volatiles present in the melt.
Degassing matters particularly in processes using recycled material, or polymers with a strong tendency to absorb moisture, because volatiles remaining in the melt can lead to bubbles, voids, or surface defects in the final product.
Why Is Degassing Critical for Moisture-Sensitive Polymers?
Hygroscopic polymers such as PET or polyamide (nylon) readily absorb moisture from the air. Even if these polymers aren't dried sufficiently before processing, the high melt temperature during extrusion can let that moisture hydrolytically break down the polymer chains — reducing the material's molecular weight and, with it, its mechanical strength.
Vacuum degassing, as a measure complementary to pre-drying, helps limit this kind of degradation by removing moisture remaining at the melt stage. This is why keeping degassing vacuum stable and sufficiently high-capacity is critical to product quality, particularly on lines processing hygroscopic polymers.
How Does Vacuum Calibration Work in Pipe and Profile Extrusion?
The pipe or profile leaving the die is still soft, not yet fully solidified. In the calibration tank, the material passes through a perforated or slotted calibration sleeve; vacuum applied outside the sleeve pulls the still-soft material outward against its inner surface, fixing it to the correct outer dimension and roundness. Cooling, via water spray or immersion, happens within the same tank.
This method is a standard technique widely used particularly in PVC, PE, and PP pipe production; the stability of calibration vacuum directly affects the final pipe's dimensional tolerance and roundness.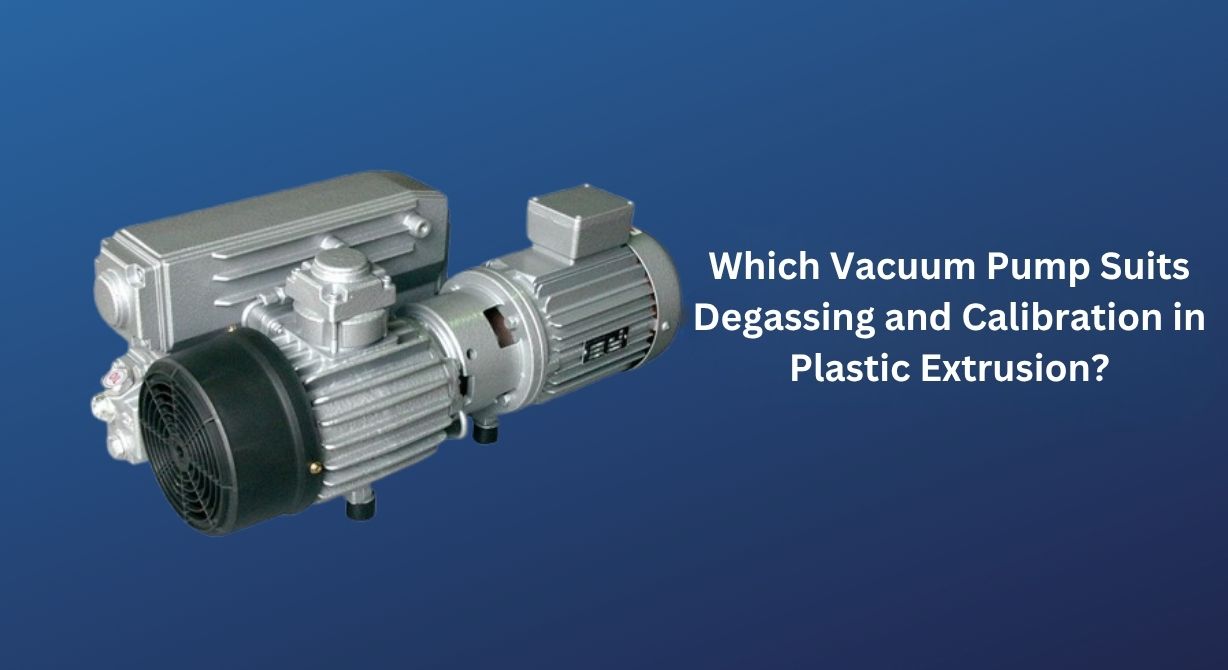
How Does the Wet Environment in a Calibration Tank Affect Pump Selection?
Because a calibration tank uses continuous water spray or a water bath to cool the material, the air drawn into the vacuum system carries a significant amount of water vapor and water droplets. As covered in our article "How Does a Liquid Ring Vacuum Pump Work?", liquid ring pumps naturally tolerate this kind of moist air stream, since the pump already carries a continuously circulating liquid.
For that reason, when selecting a vacuum pump for calibration tanks, the process's moisture load needs to stay within what the pump can tolerate; otherwise, performance loss or unwanted water accumulation inside the pump can occur.
Which Pump Technology Is Preferred for Degassing and Calibration?
Because of the moisture and vapor load involved in both degassing and calibration applications, liquid ring vacuum pumps are a widely preferred technology for both. Plastics is listed as a served sector on both Gücüm Pompa's corporate page and its ECO-SYS product page.
For certain specialized degassing applications involving a drier gas stream with less moisture, rotary vane vacuum pumps — as covered in our article "Which Applications Need the 0.5 mbar Vacuum of a Rotary Vane Pump?" — can also be considered; but that choice should be made on a project-specific basis, depending on the actual moisture load in the process.
What Protective Measures Guard Against Melt Splashing?
At the degassing port, pressure imbalance or sudden process fluctuations can occasionally cause some molten polymer to splash into the vacuum line. To prevent this risk, using a melt trap or a condenser-type separator before the vacuum pump is a common measure in general engineering practice.
A similar logic applies to the calibration tank: using a water separator or knockout device to keep water droplets from reaching the pump directly supports reliable long-term pump operation.
Frequently Asked Questions
How Deep Should Degassing Vacuum Be?
The exact value depends on the polymer being processed and the amount of volatiles that need removing; generally, a moderate and stable vacuum level is sufficient rather than an extremely deep one. Process engineering data should be the basis for a specific application.
What Problems Can Result From a Vacuum Interruption in a Calibration Tank?
A drop or interruption in vacuum level can prevent the pipe from being drawn sufficiently against the calibration sleeve, resulting in poor dimensional tolerance or roundness. That's why the stability of calibration vacuum matters for production quality.
Can the Same Pump Be Used for Both Degassing and Calibration?
These two applications generally require separate vacuum circuits, since they operate at different points, on different timing, and with different air/moisture loads. The exact system design should be determined on a project-by-project basis, according to the line's configuration.
Is Degassing Necessary for Non-Hygroscopic Polymers?
While moisture risk is lower for non-hygroscopic polymers, air trapped in the melt or volatile compounds generated during processing can still be present; for this reason, degassing is a useful step on many extrusion lines regardless of material type.